For some antimony deposits, the first opportunity is to separate barren rock before it enters the grinding circuit.
Where antimony minerals occur in coarse, sufficiently liberated particles, screening and gravity separation may produce an enriched fraction or reject part of the waste rock. This can reduce the mass requiring further treatment.
The opportunity depends on liberation and mineral distribution—not simply on a low head grade.
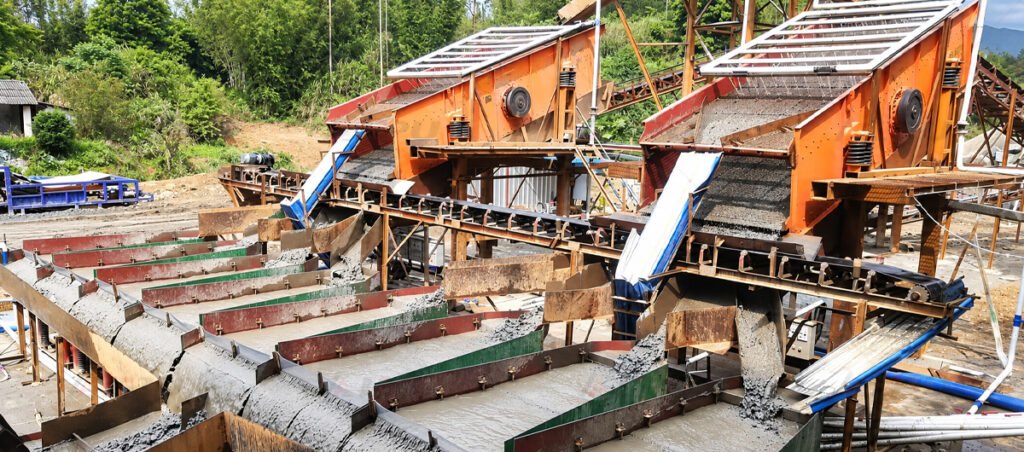
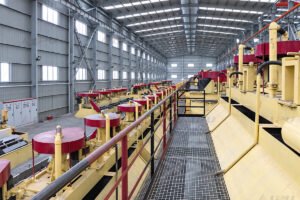
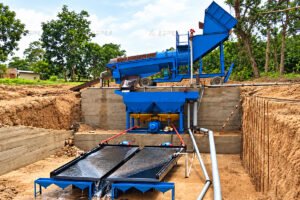
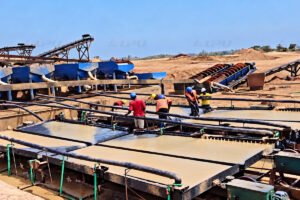
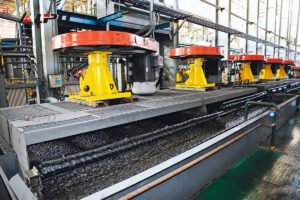
Screening and wet separation equipment at an ore processing plant
Pre-concentration testing should establish:
How antimony is distributed across particle-size fractions.
Whether valuable minerals are liberated at a coarse size.
How much mass can be rejected.
How much antimony would be lost with the rejected material.
Whether the enriched stream improves downstream processing.
A lower grinding load is useful only if the resulting metal losses and overall economics are acceptable.
Sorting may also be evaluated where mineral contrasts and feed presentation support it. Manual selection should not be treated as the default approach for every plant.
Identify the Antimony Minerals Before Selecting the Route
An antimony assay shows how much antimony is present, but not how it can be recovered.
Stibnite, oxidized antimony minerals, and complex antimony-bearing sulfides can require different treatment. Weathering, mineral locking, and associated valuable metals also influence the route.
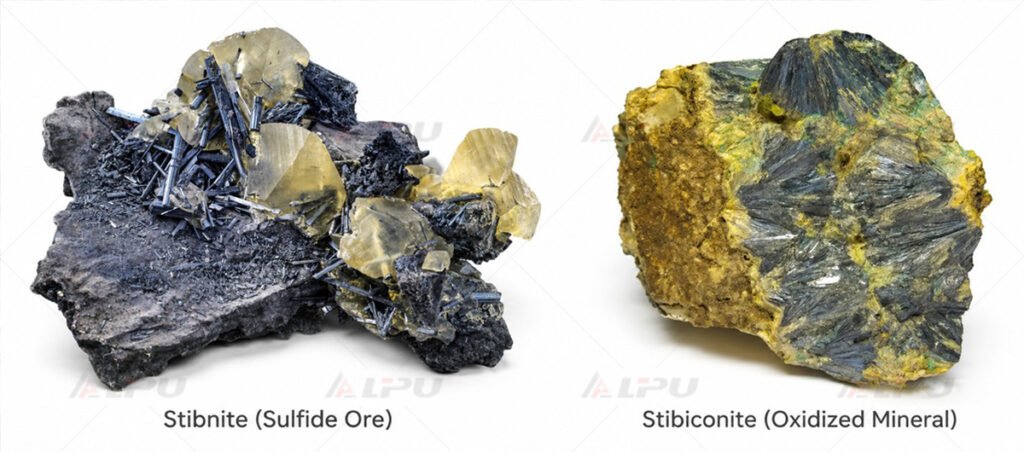
Stibnite and stibiconite specimens
Feed Characteristics
Processing Questions
Coarse, liberated stibnite with lighter gangue
Can gravity separation recover antimony or reject waste before grinding?
Fine-grained stibnite
What grind and flotation conditions provide useful recovery and selectivity?
Oxide or mixed sulfide-oxide ore
Which phases contain antimony, and how does each respond to treatment?
Gold-antimony ore
How are gold and antimony distributed, and what recovery sequence suits both products?
Complex polymetallic ore
Can separate saleable products be produced, and where do impurities report?
Oxide ore should not automatically be assigned to gravity separation. Density contrast is useful only when particle size, liberation, and material behavior allow effective separation.
Likewise, a flotation route developed for stibnite should not be assumed to recover all antimony-bearing phases.
Three Ways to Arrange the Beneficiation Circuit
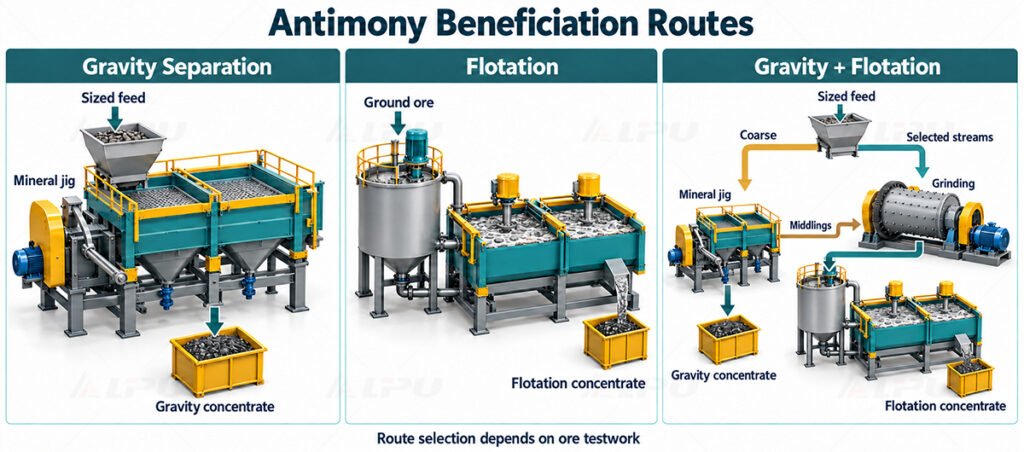
Three alternative antimony beneficiation routes
Gravity Separation for Suitable Coarse Fractions
Gravity separation can be considered where liberated antimony minerals can be separated from gangue by density.
Jigs may be evaluated for suitable coarser fractions, while shaking tables may be tested for finer classified material.
Different size fractions may need separate treatment. Middlings may require further liberation rather than repeated passage through the same separator.
The required outcome may be a finished mineral concentrate, an enriched feed for flotation, or a rejected waste fraction.
Flotation for Suitable Stibnite Feeds
Flotation is an important option for fine-grained stibnite that cannot be recovered adequately by coarse physical separation.
Grinding, reagent conditions, and cleaning stages should be selected together. The circuit must balance antimony recovery with gangue rejection and impurity control.
LIPU’s sulfide ore flotation plant solutions provide a related processing framework, with antimony-specific testwork establishing the actual operating requirements.
Gravity Separation Combined with Flotation
A combined route may suit feeds containing both coarse recoverable antimony minerals and finer material requiring flotation.
One possible arrangement is:
Crushing & Classification → Gravity Pre-concentration → Selected Streams to Grinding and Flotation → Separate Concentrate Dewatering
The gravity concentrate, middlings, and rejected streams need individual evaluation. They should not automatically be combined or sent to the same downstream operation.
Combined treatment is justified by the behavior of the material and the overall recovery—not by the number of equipment types included.
Control Liberation Without Creating Unnecessary Slimes
Antimony recovery can be affected by both insufficient liberation and excessive fines.
Locked particles may remain in tailings or contaminate concentrate. Excessive grinding can create material that is difficult to recover by gravity separation and can complicate flotation, settling, and filtration.
The preparation circuit should therefore consider:
Staged crushing with screening.
Separate treatment of appropriate size fractions.
Controlled grinding and classification.
Selective treatment of middlings.
Measurement of antimony losses in fine material.
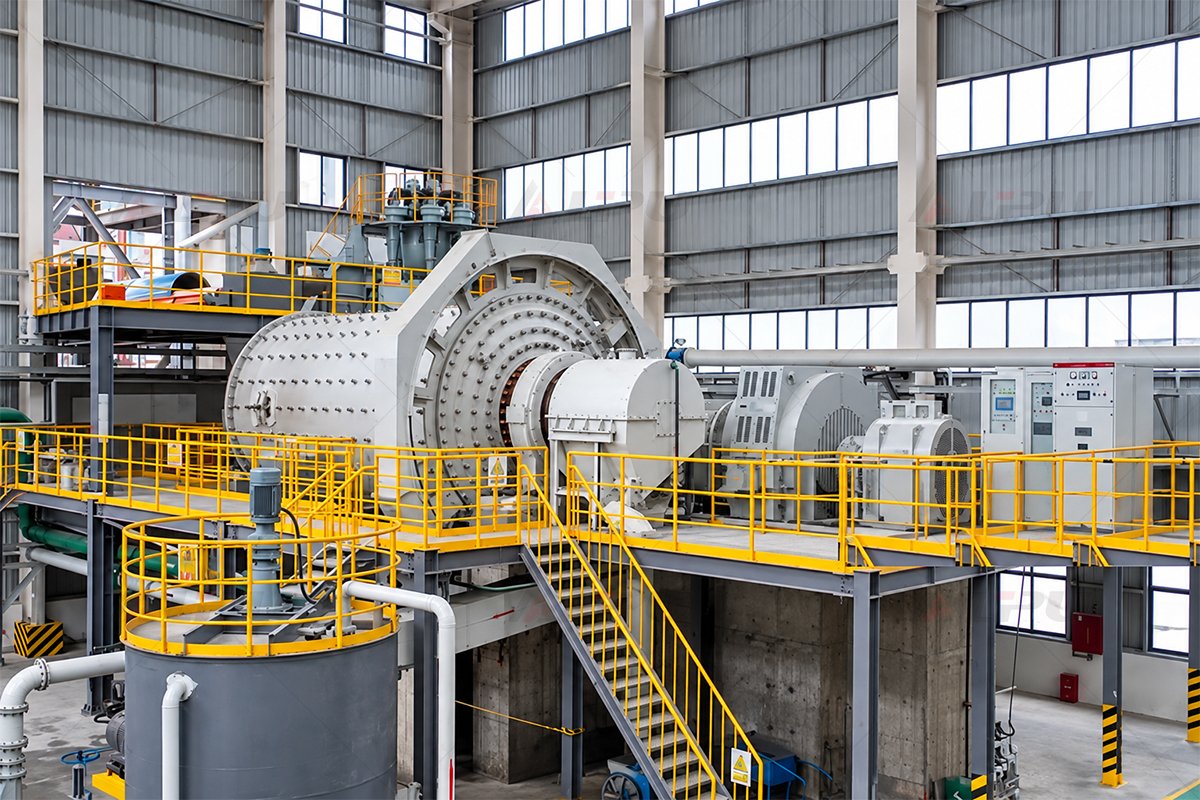
Where required, a ball mill operates with classification equipment to control the material entering flotation.
Washing or desliming may help with clay-rich feeds, but the removed fine fraction must be assayed. It should not be discarded without understanding its antimony content.
Design Around the Concentrate the Buyer Will Accept
Antimony recovery alone does not define a successful processing route.
The concentrate must also suit the receiving smelter or downstream treatment facility. Product requirements should be obtained early enough to influence separation testing and circuit design.
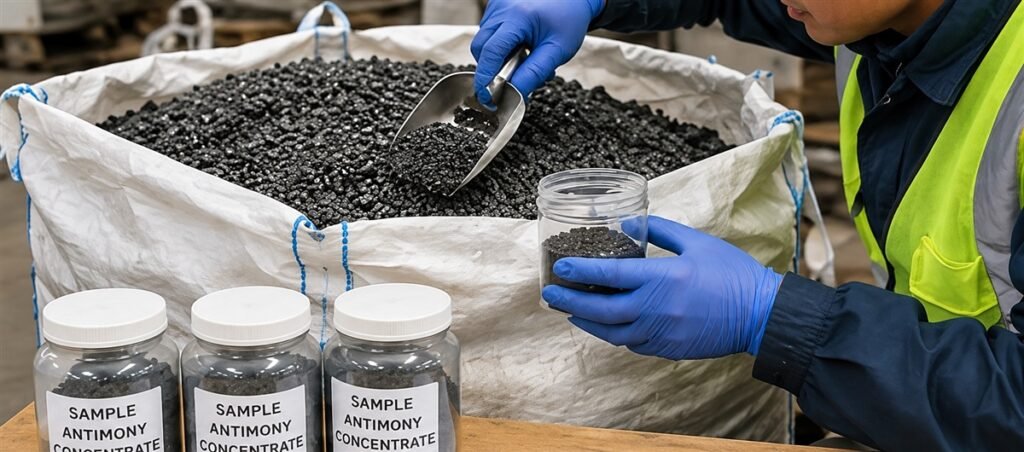
Concentrate sampling for quality testing
Product Factor
Why It Matters
Antimony grade
Influences concentrate value and downstream treatment requirements
Arsenic and other specified impurities
May affect acceptance, treatment charges, or the required processing route
Associated valuable metals
Can influence product routing and commercial terms
Moisture and physical condition
Affect handling, storage, transport, and receiving requirements
Product consistency
Determines whether the plant can supply an acceptable product across changing ore feeds
Impurity removal depends on mineral association. A separate unwanted mineral may respond to selective separation; an element contained within the recovered mineral may be much harder to reject by physical beneficiation.
The proposal should distinguish production of an antimony mineral concentrate from downstream production of antimony metal or compounds.
Investigate Tailings Losses Before Adding More Equipment
A high antimony assay in tailings does not, by itself, identify the correct recovery method.
Residual antimony may occur as:
Coarse liberated particles.
Locked particles requiring additional liberation.
Fine or oxidized minerals with a different response.
Material lost because of unstable operation or unsuitable flotation conditions.
Each cause points to a different response.
Gravity treatment of flotation tailings should only be included where testing identifies a recoverable fraction. Spiral concentrators, shaking tables, and centrifugal units are not interchangeable without testing their suitability.
A size-by-size mineral and metal balance helps determine whether to improve the existing circuit, treat a selected fraction, or evaluate a separate recovery stage.
Dewatering, Water Return and Residue Handling
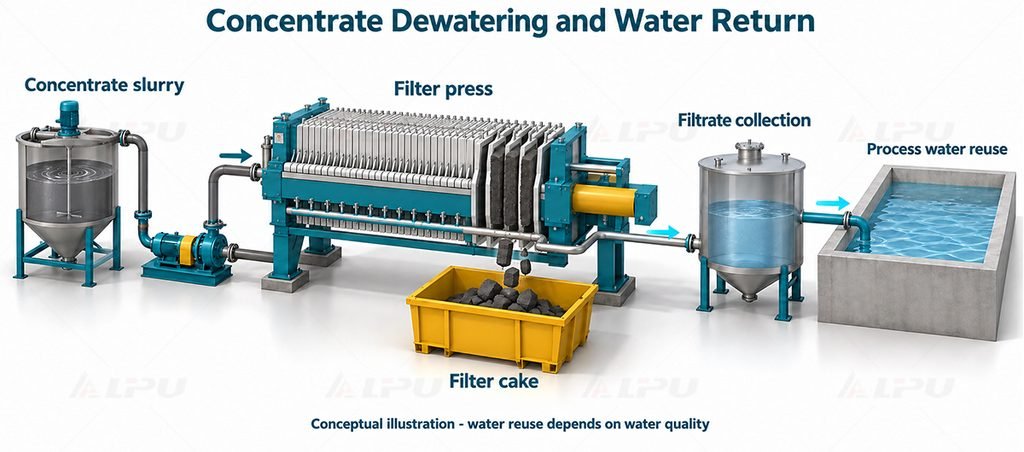
Antimony concentrates normally require solid-liquid separation before storage, transport, or further treatment.
Conceptual concentrate dewatering and water return
Thickening and filtration equipment should be selected through settling and filtration tests. Moisture removal improves handling but does not inherently increase dry-basis antimony grade.
Gravity and flotation concentrates may have different particle-size distributions and dewatering characteristics. Whether they can be combined should be confirmed against product specifications.
Process-water return should account for suspended fines, dissolved substances, and residual reagents that could affect separation.
Tailings characterization should also establish the behavior of antimony and associated elements under the proposed storage conditions. Dewatering alone does not determine residue stability or return-water quality.
What LIPU Needs to Develop a Plant Proposal
A useful proposal starts with a recovery objective and evidence about the feed.
Please provide:
Representative ore samples or available mineralogical reports.
Antimony assays and analyses of relevant impurities and associated metals.
Sulfide, oxide, and mixed-ore distribution.
Feed size, clay content, hardness, and expected variability.
Planned throughput and operating schedule.
Existing gravity, grinding, flotation, and dewatering test results.
Concentrate acceptance requirements.
Site layout, water supply, and power availability.
The resulting proposal should explain:
Which processing route is recommended and why.
Whether early waste rejection is practical.
Which streams need grinding or further treatment.
How concentrate quality will be evaluated.
How water and residues will be handled.
Which equipment duties require further testing.
LIPU uses these inputs to develop the process arrangement, equipment selection, and site configuration for the project.
Discuss Your Antimony Ore
Send LIPU your ore information, planned capacity, test results, and target concentrate requirements.
Whether the project involves coarse stibnite, fine disseminated ore, or a mixed feed, the starting point is the same: establish where the antimony occurs and which separation steps recover it into an acceptable product.
Frequently Asked Questions
Is gravity separation or flotation better for antimony ore?
Neither is universally better. Gravity separation depends on density contrast, liberation, and particle size. Flotation depends on mineral response and selectivity. Some feeds benefit from combined treatment.
Can a low-grade ore be upgraded before grinding?
Possibly. Testing must establish how much material can be rejected and how much antimony would be lost. Low grade alone does not prove that pre-concentration will work.
Can oxide and sulfide antimony ores use the same circuit?
Not automatically. Their mineral properties and processing responses may differ. Mixed feeds require testing of the individual antimony-bearing phases.
Can gold and antimony be recovered from the same ore?
Potentially, but the recovery sequence depends on mineral associations, metal distribution, and downstream product requirements. Both metals should be included in the process balance.
Should flotation tailings always pass through gravity equipment?
No. Additional gravity treatment is useful only where tailings contain particles that the selected equipment can recover effectively.
Does an antimony processing plant produce antimony metal?
The beneficiation routes described here produce mineral concentrates or enriched products. Production of antimony metal or compounds requires additional downstream treatment.