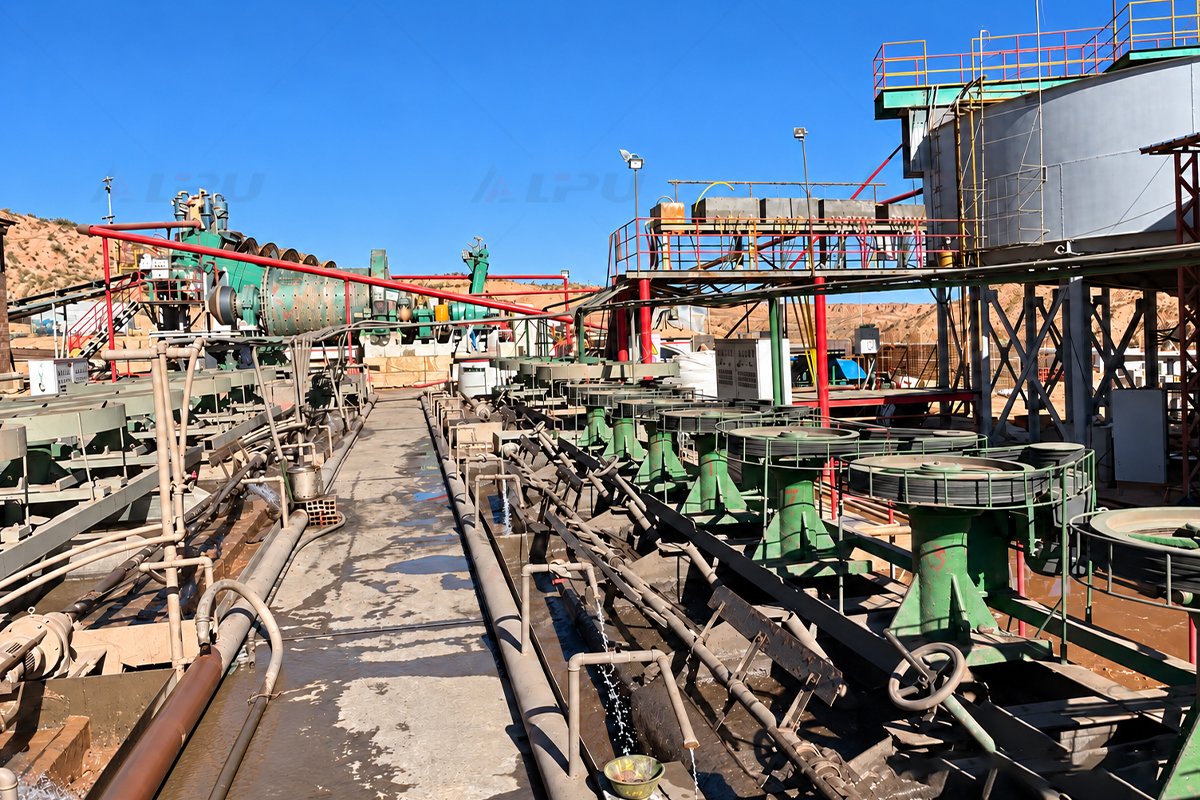
LIPU provides crushing, grinding, classification, flotation and dewatering equipment for lead-zinc ore processing.Plant configurations are tailored to the ore mineralogy, required capacity and specifications of the lead and zinc concentrates.
Send ore analysis and capacity to discuss your plant.
Recover Lead and Zinc Without Compromising Either Product
A lead-zinc plant must do more than recover two metals. It must separate them into concentrates that meet buyer requirements.
Recovering more lead offers limited benefit if excessive zinc enters the lead concentrate. Likewise, lead, unwanted iron minerals and waste rock can reduce the quality of a zinc concentrate.
The aim is to balance metal recovery, concentrate quality and operating cost. This starts with identifying the minerals carrying the lead and zinc, how closely they are intergrown, and which impurities must be removed.
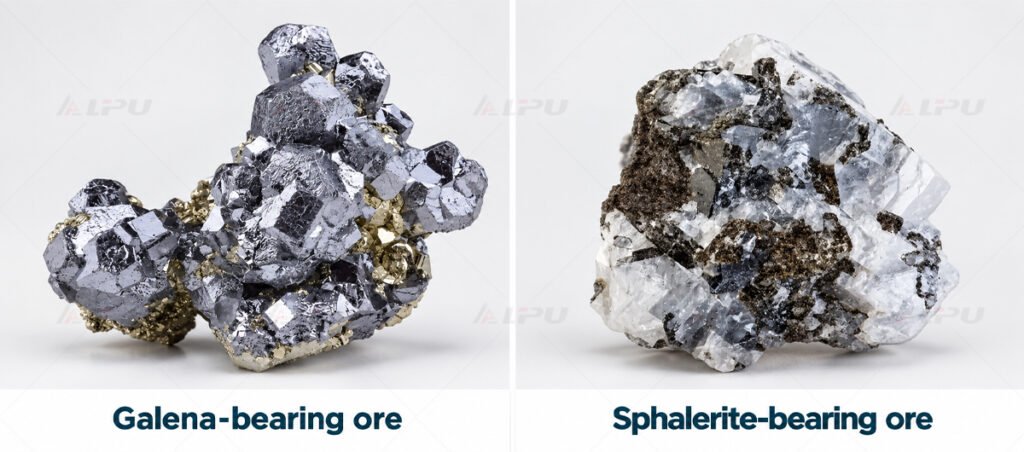
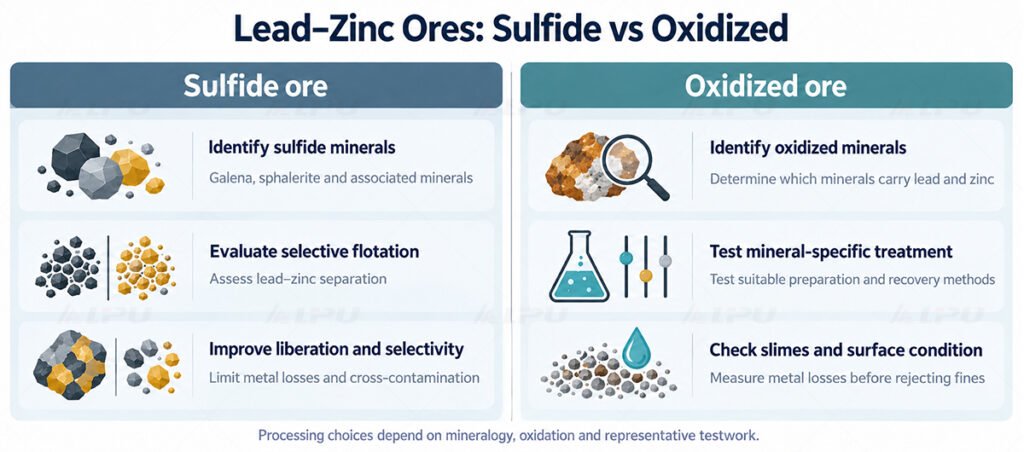
Galena and sphalerite are the principal lead and zinc sulfide minerals in many deposits. Weathering can introduce oxidized minerals that need different treatment.
Mineral composition determines the separation strategy
Feed type
Main processing challenge
What shapes the route
Sulfide lead-zinc ore
Separating galena from sphalerite and unwanted sulfides
Mineral liberation and flotation selectivity
Oxidized lead-zinc ore
Recovering minerals such as cerussite, smithsonite or hemimorphite
Mineral type, surface condition and fine material
Mixed sulfide-oxide ore
Treating minerals with different processing responses
Distribution of lead and zinc between sulfide and oxidized forms
Complex polymetallic ore
Recovering lead and zinc alongside copper or other valuable components
Additional separation duties and product requirements
Why Lead Is Often Recovered Before Zinc
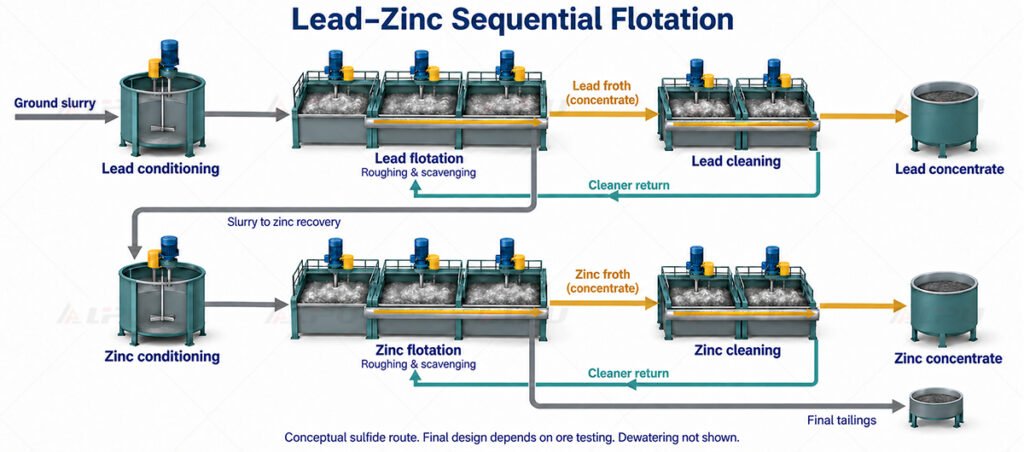
For many sulfide lead-zinc ores, sequential flotation provides a practical way to produce separate concentrates.
The lead circuit recovers galena while limiting the recovery of sphalerite and unwanted iron sulfides. Its remaining slurry then advances to zinc conditioning and flotation.
In the zinc circuit, operating conditions are adjusted to promote sphalerite recovery while controlling unwanted minerals.
The slurry leaving lead flotation is therefore not final waste—it still contains zinc to be recovered.
Each circuit may include roughing, scavenging and cleaning duties. Roughing recovers the valuable minerals, scavenging collects material missed during initial recovery, and cleaning improves concentrate quality.
Separate flotation stages recover lead and zinc products
Sequential flotation is not suitable for every ore. Where direct separation is difficult, a bulk concentrate may be recovered first and then treated to separate the lead and zinc minerals.
Flotation route
How it works
Main consideration
Sequential flotation
Lead and zinc are recovered in successive circuits
Keeping each metal in its intended concentrate
Bulk flotation followed by separation
Lead and zinc minerals are initially recovered together, then separated
Whether the bulk product can be separated efficiently
A combined route
Additional stages address copper, oxidation or complex intergrowths
Whether additional recovery justifies the added complexity
A bulk concentrate should not automatically be treated as a finished product. Its suitability depends on buyer acceptance and downstream processing.
Grind for Separation, Not Simply for Fineness
Lead and zinc minerals can occur as separate grains or remain closely intergrown with each other and with waste minerals.
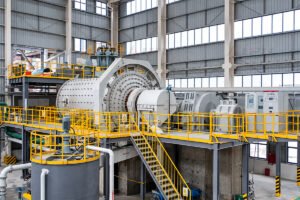
Grinding must expose enough valuable mineral for selective flotation. A ball mill can operate with classification equipment to control the size of material advancing to the flotation circuit.
There is no single grinding size suitable for every lead-zinc deposit.
A grind that is too coarse can leave lead and zinc locked together. Excessive grinding can create fine particles that are difficult to recover selectively and may increase the amount of waste material carried into the froth.
Where an intermediate product needs further liberation, selective regrinding may improve separation without grinding the entire feed more finely.
The useful result is better mineral separation—not merely a finer mill product.
Keep Zinc Out of Lead Concentrate—and Lead Out of Zinc Concentrate
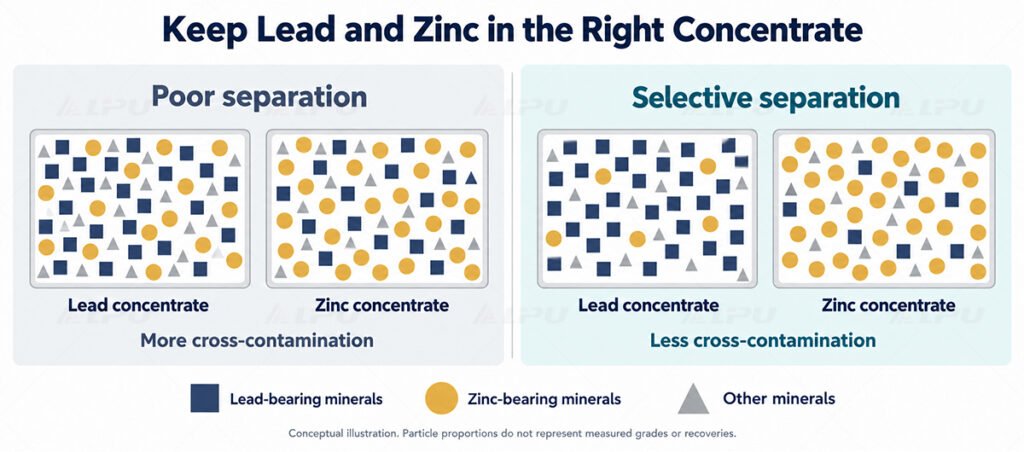
Metal recovery and concentrate quality must be assessed together. A plant can recover a high proportion of the feed metals while still producing poorly separated products.
Sphalerite floats too early or remains locked with galena
Liberation, conditioning and reagent selectivity
Excess lead in zinc concentrate
Lead recovery is incomplete or composite particles enter the zinc circuit
Lead circuit performance and selective regrinding
High iron in either product
Iron-bearing minerals enter the concentrate, or iron occurs within sphalerite
Mineral composition and the limits of physical cleaning
Excess silica or other waste minerals
Locked particles or fine waste are carried into the froth
Classification, liberation and froth control
Unstable product quality
Feed composition, water quality or operating conditions vary
Blending, sampling and operating consistency
Cleaning stages remove unwanted minerals from recovered material, but they can also lose valuable lead or zinc. Their performance should therefore be judged by both the quality gained and the metal lost.
LIPU flotation machines can be arranged for roughing, scavenging and cleaning duties according to the required separation.
Product acceptance also depends on more than lead or zinc grade. Buyer specifications may include limits for cross-contamination, impurities and moisture, together with conditions for payable associated metals.
Silver may accompany galena, while copper-bearing minerals can require additional separation. Their distribution should be measured in the actual products.
Barite or other by-product recovery is only considered where the ore composition, recovery potential and market justify it. It is not a standard stage in every lead-zinc plant.
Give Oxidized Ore Its Own Treatment Plan
A flotation circuit developed for fresh sulfide ore should not be assumed to recover oxidized lead and zinc minerals effectively.
Oxidized feeds can contain several different lead and zinc minerals. Weathered surfaces, clay and very fine material can further change the processing response.
Depending on the mineral composition, testing may evaluate specialized flotation conditions, controlled sulfidization or other treatment methods.
Oxidized ores require a mineral-specific treatment approach
The assessment should establish:
How much lead and zinc occurs in sulfide and oxidized forms.
Which minerals carry the recoverable metal.
How recovery changes across particle sizes.
Whether a suitable concentrate can be produced consistently.
How much valuable material remains in slimes and tailings.
Desliming requires particular care. Removing fine material may improve flotation conditions, but it can also discard recoverable lead or zinc.
Recovery expectations should reflect the ore that will actually enter the plant, including changes in weathering and oxidation.
Protect Product Quality During Dewatering and Water Reuse
Lead and zinc concentrates normally require dewatering before storage or dispatch.
Each product needs a clearly defined collection and handling arrangement to prevent mixing. This may involve dedicated equipment or an operating arrangement that keeps the products separate, depending on plant scale and production requirements.
Concentrates are thickened where necessary and filtered to meet the required handling and moisture conditions. Equipment selection depends on their settling and filtration behavior.
Thickening and filtration remove water. They do not replace flotation cleaning or remove impurities locked within mineral particles.
Collected water may be reused after checking its suitability. Dissolved substances, suspended solids and residual reagents can affect the selectivity of the lead and zinc circuits.
Tailings need a separate handling and water-management arrangement suited to their composition and site conditions. Additional concentrate drying is included only when required by transport conditions, the buyer or downstream treatment.
Choose Equipment That Supports Clean Separation
The equipment must work as a connected system. Consistent crushing feed supports stable grinding, controlled grinding supports flotation, and suitable cleaning protects the quality of both concentrates.
A jaw crusher can provide primary size reduction. Further crushing and screening are selected according to ore hardness, feed size and the required mill feed.
Plant section
Equipment to evaluate
Main selection priority
Feed preparation
Feeders, crushers and screens
Consistent feed and suitable size reduction
Grinding and classification
Ball mill, hydrocyclones or classifiers
Liberation and control of flotation feed size
Conditioning
Agitated tanks and reagent systems
Controlled preparation for each flotation duty
Lead flotation
Roughing, scavenging and cleaning cells
Lead recovery with limited zinc contamination
Zinc flotation
Conditioning and flotation cells
Zinc recovery with control of lead and unwanted minerals
Selective regrinding
A suitable mill and classification arrangement
Liberation of intermediate products where necessary
Concentrate dewatering
Thickeners, filters and product-handling equipment
Moisture control and prevention of mixing
Gravity or magnetic separation may have a supporting role where a specific mineralogical feature justifies it. Neither should be added to every lead-zinc flowsheet by default.
Plant layout should also allow access for maintenance, sampling and inspection, particularly around mills, flotation cells, pumps and filters.
Plan Your Plant Around the Ore
A useful proposal starts with the information that affects separation and equipment duty.
Provide:
Lead and zinc assays, with available impurity analysis.
Mineralogical information and the degree of oxidation.
Required capacity and operating hours.
Feed size and available grinding data.
Previous metallurgical test results.
Target lead and zinc concentrate specifications.
Information on silver, copper and other associated values.
Site water, power, space and operating conditions.
Representative samples should cover the main ore types expected during operation. For an existing plant, separate assays of both concentrates, intermediate streams and final tailings help locate the main losses.
Contact LIPU with your ore information to discuss equipment and process options for your project.
Frequently Asked Questions
Why do lead and zinc usually need different flotation conditions?
The circuits have different separation duties. The lead stage aims to recover galena while limiting sphalerite recovery; the zinc stage then adjusts conditions to recover sphalerite from the remaining slurry.
Is lead always recovered before zinc?
No. Lead-first sequential flotation is common for suitable sulfide ores, but bulk flotation followed by separation or a more complex arrangement may be appropriate for other feeds.
Can oxidized ore use the same conditions as sulfide ore?
Not without verification. Oxidized minerals can require different surface treatment, reagents and feed preparation.
Does adding more reagent improve recovery?
Not necessarily. Excess reagent may recover more unwanted minerals or interfere with subsequent separation. The objective is selective recovery rather than maximum froth production.
What concentrate grades and recoveries can the plant achieve?
Credible targets require representative testing, an agreed feed range and defined product specifications. Results from another deposit should not be used as a guarantee.